Global sourcing teams rarely choose molded packaging for appearance alone. They examine protection, cost, materials, production capacity, and delivery reliability. A tray that fits perfectly in a sample room may fail after weeks in humid sea freight. Small details matter. Corners can crush. Stacking pressure can distort cavities. Temperature changes can weaken performance.
Walter Soroka, a respected packaging educator and author of Fundamentals of Packaging Technology, described packaging as “the art, science, and technology of enclosing and protecting products for distribution, storage, sale, and use.” His definition remains practical for international buyers. Molded packaging must protect the product, support efficient handling, and communicate responsible material choices. It also needs measurable specifications, not attractive promises.
This guide presents ten practical tips for evaluating molded packaging across global supply chains. It considers fiber, pulp, plastic, and other molded formats. The discussion covers fit, cushioning, tooling, moisture exposure, testing, labeling, logistics, and supplier verification. It also addresses questions buyers sometimes overlook, such as mold ownership and replacement timelines.
No packaging decision is perfect.
A lower-cost design may require stronger outer cartons. A sustainable material may need moisture protection. A supplier with excellent samples may lack stable mass-production controls. These trade-offs deserve honest review. Buyers should request test data, inspect production samples, and confirm tolerances before approving large orders. Regional recycling systems also differ, so a material described as recyclable may not be widely accepted locally. Careful questions reduce surprises. Careful documentation builds trust.
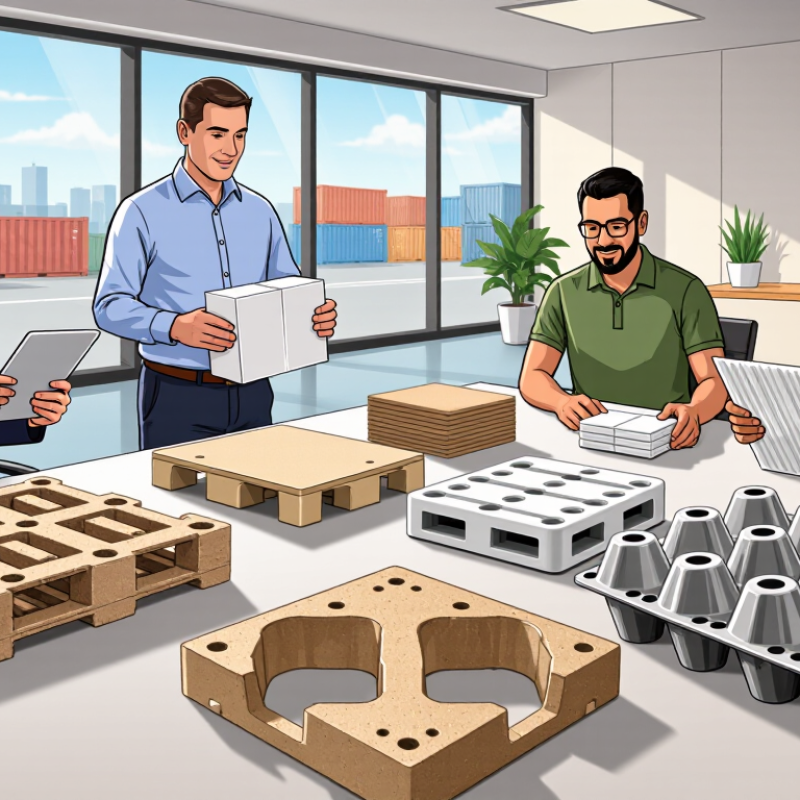
Start with the product, not the package. Fragile electronics may need rigid pulp inserts or thermoformed trays. Fresh food often requires molded fiber with moisture-resistant treatment. Heavy industrial parts may need compression-molded supports or engineered foam cushions. Match the material to impact, weight, temperature, and contact requirements.
Check cavity dimensions carefully. A small gap can cause movement during ocean transport. Test humidity, vibration, stacking pressure, and repeated handling. Do not trust a laboratory result alone. Real shipping lanes can be harsher. Molded fiber performs well for many retail and food applications, but high humidity may weaken it. Thermoformed plastic offers accurate shapes, although its recycling route differs between countries. A perfect material rarely exists.
Review local recycling rules before approving the design. Confirm food-contact, labeling, and restricted-substance requirements in every target market. Ask suppliers for material specifications, test records, and tooling tolerances. Plan for spare molds when production crosses regions. Keep the design simple. Complex cavities can increase damage, cleaning, and replacement costs. Pilot shipments reveal problems early, especially with stacking and customs handling. I have seen packaging pass drop tests yet fail after several damp warehouse days. That result deserves a design review, not excuses. Use clear drawings, consistent measurements, and documented acceptance criteria.
Molded packaging must protect the product before it supports a sustainability claim. Check one: identify impact points, corners, screens, and fragile closures. Check two: match cushioning thickness with product weight and drop height. Check three: test compression under stacked cartons. Check four: measure vibration performance during simulated road and air transport. Check five: examine moisture resistance, especially for molded fiber. Check six: compare dimensional tolerances across production batches. Small variations can create movement. Use ISTA-style distribution testing, not only a controlled drop test. The OECD Global Plastics Outlook reports that 353 million tonnes of plastic waste were generated in 2019, while only 9% was recycled. Material efficiency now deserves equal attention.
Check seven: review density, recovery, and permanent deformation after compression. Check eight: inspect fiber bonding or foam cell structure under magnification.
Check nine: confirm that surface contact will not scratch, stain, or abrade the product. Check ten: verify performance after temperature and humidity conditioning.
A package may pass dry testing and fail in a humid container. It happens.
For global purchasing, request test methods, sample sizes, conditioning details, and failure photos. Compare performance per gram of material, not packaging weight alone. ISO 18601 guidance supports evaluating packaging throughout its life cycle. Still, recyclability claims can be incomplete when coatings, adhesives, or mixed materials complicate recovery. A lower-cost design may also require more replacement shipments.
The overlooked question is simple: does the package protect the product reliably in real handling?
10 Molded Packaging Tips for Global Buyers
Matching Packaging Design to International Shipping Conditions
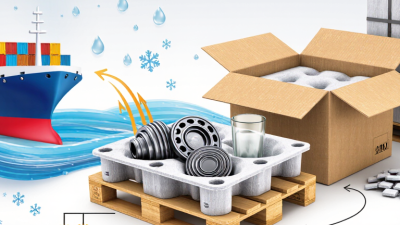
Molded packaging must survive more than a warehouse drop. It may face vibration, salt air, humidity, compression, and rapid temperature changes. UNCTAD reports that over 80% of global merchandise trade by volume moves by sea. That makes moisture resistance and stable stacking essential for international shipments. A molded fiber tray may protect a product well inland, yet soften after days in a humid container. Add a water-resistant coating when testing proves it necessary.
Design around the route, not only the product. Measure the item’s weight, fragile points, center of gravity, and clearance before creating the mold. Use ribs, corner supports, and controlled crush zones to spread impact. Keep empty space low, but allow enough tolerance for manufacturing variation. Packaging tests should include compression, vibration, shock, and climate conditioning. ISTA test procedures provide a practical framework for these checks. Real samples matter.
World Bank research estimates that global municipal waste reached 2.01 billion tonnes in 2016. Material reduction therefore deserves attention, not just protection. Recycled molded fiber can lower material use, but performance may vary between suppliers and climates. I have seen elegant prototypes fail because damp trays warped during loading. That mistake is avoidable, though not always obvious. Request production samples, inspect seams, and repeat tests after storage. A design that passes once is not automatically reliable.
Global molded packaging buyers should verify rules before approving a production sample. Requirements may change by destination, material, and product contact. Ask suppliers for resin identification, food-contact declarations, chemical test reports, and manufacturing traceability. Keep records. A batch code, production date, and supplier address can make investigations faster. Check package dimensions too, because oversized formats may create transport or waste concerns.
Labels need careful review. Confirm required languages, country-of-origin statements, recycling symbols, handling instructions, and warning text with a qualified local specialist. Do not guess. A symbol accepted in one market may confuse buyers elsewhere. Printed claims such as “recyclable,” “compostable,” or “made with recycled content” should match test evidence and documented percentages. Small errors spread across thousands of units.
Sustainability checks should include material weight, recycled content, energy use, and end-of-life conditions. Recyclability on paper may fail where collection systems are limited. Ask for migration testing when packaging touches food, cosmetics, or other sensitive products. Request recent certificates, not copied files from an earlier project. Supplier audits can reveal weak controls, although audits are not perfect. A useful improvement is reviewing packaging after real shipment, where crushing, moisture, and label wear become visible. Local regulations and interpretations can still change, so buyers should schedule periodic compliance reviews.
10 Molded Packaging Tips for Global Buyers
Comparing suppliers starts with the product, not the quotation. Ask for material data, wall-thickness limits, and sample approval procedures. A capable supplier should explain tooling life, cavity design, and expected production tolerance. Request samples from actual production equipment. Samples made by hand can hide defects.
Compare the full landed cost, including molds, packaging, freight, duties, inspection, and possible rework. The lowest unit price may carry higher waste or tooling charges. Ask whether prices change with order volume and resin fluctuations. Check payment terms carefully. They affect cash flow. Quality requires measurable standards, such as weight tolerance, dimensions, surface finish, and drop-test performance. Use a written inspection plan with clear acceptance limits.
Delivery capability deserves equal attention. Review monthly capacity, backup equipment, holiday schedules, port options, and production lead times. Ask for a realistic timeline from design approval to shipment. A supplier that promises everything immediately may be guessing. Keep a small schedule buffer for mold corrections and customs delays. Verify certifications and traceability documents when the product requires them. Video audits help, but they cannot replace independent inspection. No comparison is perfect. I would revisit the scoring after the first shipment, because real performance often exposes weaknesses that spreadsheets miss.
A practical comparison framework for molded pulp, molded fiber, and molded protective packaging sourcing.
| Buying Tip | What to Compare | Typical Planning Data | Quality Evidence to Request | Delivery and Cost Considerations | Buyer Assessment |
|---|---|---|---|---|---|
| 1 Define the application first | Product weight, drop height, stacking load, moisture exposure, temperature, and contact requirements. | Common molded-fiber packaging applications include product trays, end caps, inserts, and protective corner pieces. | Request a written specification covering dimensions, mass, wall thickness, compression requirements, and acceptable cosmetic defects. | A precise specification reduces tooling changes, sampling delays, and unexpected material use. | High priority |
| 2 Compare the total landed cost | Unit price, tooling, sampling, packaging, freight, duties, inspection, storage, and payment terms. | Tooling is commonly quoted separately; total cost can differ significantly when bulky molded parts are shipped long distances. | Ask for a costed bill of materials, tooling ownership terms, packaging method, and quotation validity period. | Compare cost per packed product, not only cost per molded component. Ocean freight generally costs less than air freight but requires longer planning. | Mandatory |
| 3 Check material consistency | Fiber source, recycled content, additives, moisture level, density, color, odor, and batch variation. | Recycled paper fibers and agricultural fibers may vary in length, cleanliness, moisture absorption, and surface finish. | Request a material declaration, batch test records, restricted-substance statement, and retained samples from production lots. | More consistent raw material usually improves yield and reduces rejects, although it may increase material cost. | High priority |
| 4 Verify dimensional capability | Part dimensions, fit, wall thickness, draft angle, flatness, burrs, warpage, and tolerance control. | Dry molded-fiber parts generally require more generous tolerances than injection-molded plastic parts because fiber, moisture, and drying affect dimensions. | Require a dimensioned drawing, inspection plan, calibrated measuring equipment, and first-article inspection report. | Tighter tolerances may require additional tooling refinement, machining, inspection, or secondary processing. | Fit-critical |
| 5 Test mechanical protection | Compression strength, edge crush resistance, cushioning, vibration response, and impact performance. | Protection performance depends on geometry, density, moisture condition, product mass, and carton design—not material type alone. | Request test samples and reports for compression, drop, vibration, and climate conditioning where relevant. Use recognized packaging test methods. | Testing should be performed with the actual product, inner pack, and shipping carton because isolated component tests may not represent field performance. | Test required |
| 6 Evaluate moisture resistance | Humidity exposure, water absorption, barrier coating, storage environment, and recycling impact of additives. | Uncoated molded fiber is generally moisture-sensitive; humidity can affect strength, dimensions, and surface appearance. | Request water absorption or Cobb testing where applicable, humidity-conditioned compression data, and coating composition details. | Coatings can improve moisture performance but may affect recyclability, cost, odor, and end-of-life sorting. | Application dependent |
| 7 Audit production capacity | Installed equipment, available shifts, mold count, drying capacity, labor coverage, maintenance, and backup plans. | Capacity is often constrained by forming, hot pressing, drying, trimming, and inspection rather than by forming equipment alone. | Request a production-flow diagram, monthly capacity calculation, recent utilization level, and contingency plan for equipment downtime. | Confirm whether quoted capacity is dedicated to the program or shared with other orders during peak periods. | Capacity check |
| 8 Build a realistic lead-time plan | Design approval, tooling, sampling, testing, production, inspection, export documentation, and transit time. | A typical new molded-packaging program may require several weeks for tooling and validation, followed by production and international transit. | Request a milestone schedule with responsible parties, approval gates, sample quantities, and a defined date for production release. | Include buffer for tooling corrections, public holidays, port congestion, customs clearance, and final-mile delivery. | Schedule critical |
| 9 Confirm quality control systems | Incoming inspection, in-process checks, final inspection, defect classification, traceability, and corrective-action process. | Important controls include dimensions, weight, moisture, appearance, fit, compression performance, and packaging cleanliness. | Request inspection records, calibration certificates, sampling levels, nonconformance reports, and a documented corrective-action procedure. | Independent pre-shipment inspection can reduce risk, but it should supplement—not replace—supplier process controls. | Risk reduction |
| 10 Review sustainability claims carefully | Recycled or renewable content, recyclability, compostability claims, coatings, inks, water use, and waste management. | Environmental performance depends on feedstock, energy source, additives, transport distance, use phase, and local recycling or composting infrastructure. | Request third-party certifications where required, chain-of-custody documents, material declarations, and substantiation for environmental claims. | Choose claims that match the destination market’s labeling rules and actual disposal infrastructure; avoid unsupported terms such as “100% eco-friendly.” | Verify locally |
Planning note: Cost, capacity, tolerance, and lead-time figures for molded packaging vary with part geometry, fiber composition, tooling design, order volume, testing requirements, destination, and shipping method. Use this table as a supplier-comparison checklist and validate all figures through samples, documented tests, and a written quotation.