China Top Footwear Inspection Services for Global Buyers
China has become a critical sourcing hub for global footwear buyers. The World Footwear Yearbook 2024 reported more than 22 billion pairs produced worldwide in 2023. A small defect can therefore affect thousands of pairs, not just one shipment.
Footwear Inspection helps buyers verify materials, workmanship, sizing, packaging, and production consistency before goods leave the factory. Inspectors may examine loose threads, uneven bonding, color variation, heel alignment, and carton markings. They can also compare finished shoes against approved samples and technical specifications. Small defects matter. They can trigger returns, delays, or customer complaints.
Quality expert W. Edwards Deming offered a useful warning: “Quality comes not from inspection, but from the improvement of the production process.” His principle remains highly relevant to footwear sourcing. Inspection should not replace supplier development, clear specifications, or process control. It should reveal where those systems are failing.
China’s footwear supply chain is extensive, but factory capability can vary sharply. Some facilities use automated cutting and digital production records. Others still depend heavily on manual assembly and visual checks. This creates both strength and uncertainty. A report may look complete while sampling still misses hidden defects.
Professional inspection providers should use documented checklists, AQL-based sampling, calibrated tools, photo evidence, and traceable reporting. SATRA testing guidance can also support evaluations of footwear performance and material behavior. These practices improve reliability, though no inspection plan is perfect.
For global buyers, selecting China Top Footwear Inspection Services means looking beyond price. Experience, technical competence, transparent evidence, and consistent communication matter more. A dependable inspection partner turns factory observations into practical decisions before shipment.
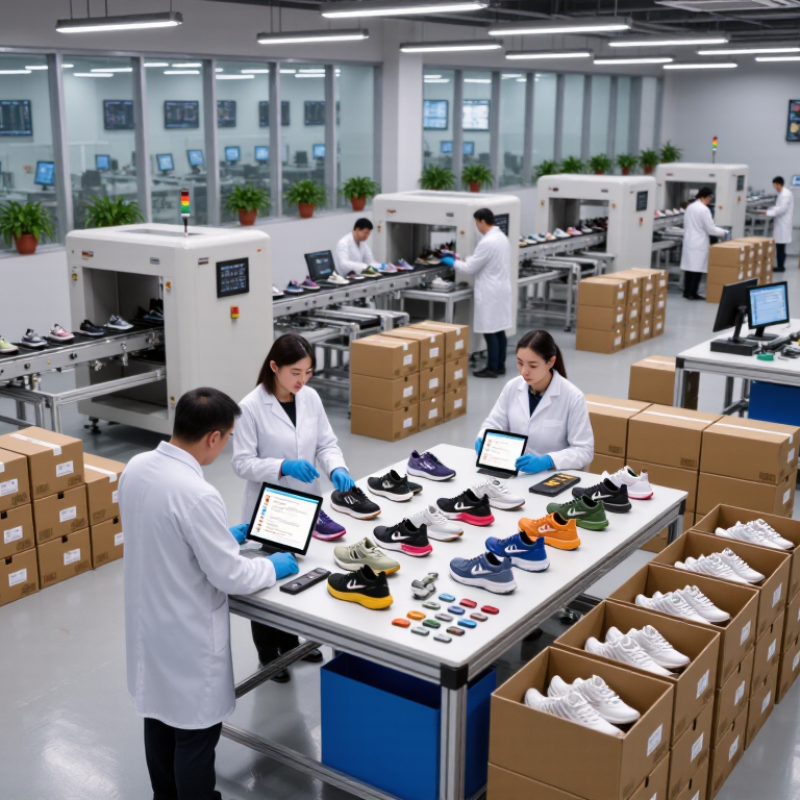
What China Footwear Inspection Services Include
China’s footwear inspection services help global buyers control quality before cartons leave the factory. The World Footwear Yearbook 2024 reported about 22.4 billion pairs produced worldwide in 2023. China accounted for approximately 55.5% of that output, making consistent factory verification especially important.
Inspection usually begins with a pre-production review. Inspectors compare approved samples, materials, size charts, color references, and packaging instructions. During production, they check stitching density, glue coverage, outsole alignment, surface marks, and shade variation. A final random inspection then measures workmanship, dimensions, labeling, carton quantity, and functional details. Sampling can follow ISO 2859-1, with defect limits agreed before inspection starts.
Some services add laboratory testing. Common checks include sole bonding strength, flex resistance, color migration, slip performance, and material composition. Results should include photographs, sample quantities, defect classifications, and corrective-action notes. A loose thread near the heel may seem minor, but repeated defects can affect returns and customer trust. A clean inspection is not a guarantee. Hidden moisture, rushed repairs, or weak bonding may appear later. That is why experienced inspectors sometimes revisit production records and compare findings across batches. Small inconsistencies deserve attention.
When Global Buyers Need Footwear Inspections
Global buyers need footwear inspections when product specifications, factory records, or shipment risks are unclear. A reliable inspection can begin before production, when materials and approved samples are checked. It can continue during production, especially after cutting, stitching, and sole attachment. Final random inspections help confirm quantities, workmanship, packaging, and carton markings before shipment.
In practice, inspectors examine size measurements, color consistency, stitching density, adhesive coverage, sole bonding, surface defects, and odor. They compare findings with the buyer’s specification sheet and approved reference sample. For safety-related footwear, suitable laboratory testing may verify physical performance and material requirements. Inspectors should also record photographs, sample sizes, defect classifications, and factory conditions. Clear evidence matters.
Timing can change the result.
A pre-shipment inspection is useful when production is nearly complete, but it may leave little time for corrections. An inline inspection can identify repeated problems earlier, although production may not yet represent the final shipment. No inspection catches everything. Small issues can escape during rushed sampling or unclear communication. Buyers should review reports carefully, question unexplained results, and define acceptance standards before production begins. Independent inspectors with footwear experience can provide more consistent judgments, yet their work still depends on accurate documents and honest factory access. That limitation deserves attention.
How a China Footwear Inspection Is Planned and Conducted
China Top Footwear Inspection Services for Global Buyers
How a China Footwear Inspection Is Planned and Conducted
A reliable China footwear inspection starts before production ends. The buyer shares specifications, approved samples, size ranges, packaging rules, and shipment targets. An experienced inspector converts these details into a practical checklist. The plan defines the factory location, inspection date, sampling level, and defect limits. It also identifies critical points, including outsole bonding, stitching tension, color consistency, and carton markings. Clear evidence matters. Photos should show the whole shoe, close defects, labels, and measurements beside a calibrated ruler.
During the visit, the inspector verifies production status and counts finished, packed, and unfinished pairs. Random cartons are opened across the lot, not only from convenient stacks. Each selected pair is checked for appearance, dimensions, workmanship, function, and packing accuracy. Simple tests may include flexing the sole, checking lace strength, and comparing colors under suitable light. Findings are recorded with sample numbers and images. An honest report also notes limitations. A visual inspection cannot prove long-term durability. Sampling can miss a rare defect. That is worth admitting.
Tips: Send the latest specification before booking. Keep defect definitions measurable. Ask for carton-level photos and a clear pass, hold, or fail decision. Recheck recurring issues after corrective work; one repaired pair does not prove the whole lot is fixed. Small omissions happen, even in careful inspections.
Which Quality Standards and Tests Are Commonly Used
China Top Footwear Inspection Services for Global Buyers
Reliable footwear inspections usually combine visual checks, measurements, and laboratory testing. Inspectors often use ISO 2859-1 sampling plans with an agreed AQL level. They examine stitching, glue marks, wrinkles, color differences, and surface damage. Small defects matter. Measurements include length, width, weight, heel height, and outsole thickness. A calibrated gauge helps reduce inconsistent decisions between inspectors.
Common performance tests include outsole flexing, abrasion resistance, bond strength, slip resistance, and colorfastness. Inspectors may rub a shoe upper with dry and wet cloths to check color transfer. They can also test adhesive strength between the upper and sole.
For children’s footwear, sharp edges, small detachable parts, and material safety require closer review. Testing should follow the buyer’s specification and suitable ISO, ASTM, or EN methods. Standards alone are not enough.
During factory inspections, I prefer reviewing production samples beside the approved reference sample. This reveals differences that a checklist may miss. Yet visual grading can remain subjective, especially with leather texture or hand-finished details. That is a weakness worth recording.
Clear defect photos, measurement records, sample quantities, and test conditions make reports more reliable. A shipment may pass appearance checks but fail flexing after repeated movement. Factory staff should investigate the cause, not only repair visible defects. Good inspection work connects test results with actual shoe use.
How to Choose a China Footwear Inspection Provider
Choosing a China footwear inspection provider requires more than comparing daily fees. The World Footwear Yearbook 2024 estimates that global production reached 22.4 billion pairs in 2023. China produced about 55.5% of them. Scale increases the value of consistent inspections.
Check the provider’s inspector training, footwear experience, and independence from factories. Ask whether reports follow ISO 2859-1 or ANSI/ASQ Z1.4 sampling methods. An AQL 2.5 level is common, but it is not a guarantee of zero defects. Define critical, major, and minor defects clearly. Inspectors should examine stitching, bonding, sizing, color, labeling, packaging, and odor. They should also photograph defects beside a ruler.
Technical testing matters for leather, rubber, adhesives, and children’s footwear. Select laboratories accredited to ISO/IEC 17025 when chemical or performance tests are required. The OECD’s Due Diligence Guidance for Responsible Supply Chains also supports traceable supplier information and documented risk controls. Request sample reports, inspector qualification records, response times, and corrective-action follow-up.
Do not choose by price alone. A low quote can look efficient. It may not be. I have seen reports with many photographs but weak defect descriptions, making factory correction difficult. Test the provider with one production lot first. Review accuracy, clarity, and whether findings match your approved sample. A useful provider should challenge unclear specifications, not simply complete a checklist.

 English
 Polski
 Čeština