Choosing the right box can shape how customers view your product before they open it. Custom corrugated packaging offers more than attractive printing. It can protect fragile items, control shipping costs, and create a consistent brand experience.
In real packaging projects, small details often cause expensive problems. A box may look strong but collapse under stacking pressure. A beautiful design may waste interior space or require costly inserts. Measuring the product, testing the board grade, and checking closure strength can prevent these issues. Fit comes first. Even a few extra centimeters can increase material use and delivery charges.
This guide shares ten practical tips for choosing custom corrugated packaging with greater confidence. It considers product weight, dimensions, flute profiles, printing methods, moisture exposure, and expected handling conditions. These factors should be evaluated together, not separately. A lightweight carton may suit retail shelves but fail during long-distance transport. A premium finish may impress customers but offer little value for a low-margin product.
Experience also teaches humility. Packaging tests cannot predict every warehouse or courier condition. Still, drop tests, compression checks, and sample shipments provide useful evidence. Speaking with a qualified packaging supplier can reveal weaknesses that drawings conceal. Reliable decisions come from balancing protection, appearance, sustainability, and budget. The best package is not always the most elaborate one. It is the one that performs consistently, communicates clearly, and respects real operating conditions.
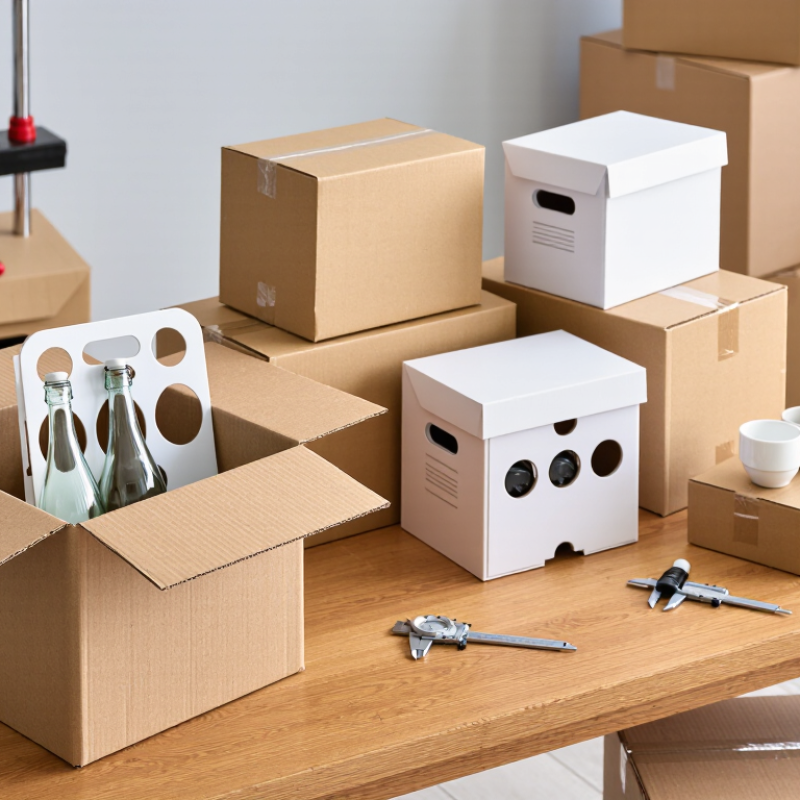
Tip 1: Measure the product before discussing box designs. Record its length, width, height, weight, and fragile points. Include protective materials in the measurements. A few extra millimeters can affect fit, shipping cost, and stability.
Tip 2: Decide what the package must achieve. Is the priority impact protection, easier storage, lower material use, or stronger shelf presentation? These goals can conflict. A lightweight box may reduce expenses but provide less protection during rough handling. I have seen packaging fail because teams focused only on appearance.
Tip 3: Describe the shipping environment clearly. Note stacking height, delivery distance, humidity, temperature changes, and likely handling pressure. A box for warehouse storage needs different performance from one sent directly to a customer. Corrugated strength should match real conditions, not assumptions.
Tip 4: Build a simple testing plan. Check compression, edge strength, drop resistance, and product movement inside the box. Use a filled sample, not an empty carton. The first prototype may look convincing and still perform poorly. That is normal.
Tip 5: Define measurable objectives. For example, the product should remain undamaged after repeated handling, and the package should close without excessive tape. Write these requirements before selecting board grade or printing details. Otherwise, design discussions can become subjective and slow.
Tip 6: Leave room for honest review. Product weights may change, and warehouse conditions may be misunderstood. Recheck the specifications with production and logistics teams before approving the final structure. Small oversights become expensive later.
Choosing custom corrugated packaging starts with the material, not the printed design. I have seen attractive boxes fail because their liners were too weak for humid storage. Kraft liners usually provide cleaner surfaces and reliable tear resistance. Recycled liners can perform well, but their quality varies by supplier and moisture level. Ask for material specifications, not vague claims about “heavy duty” strength.
Box strength should match the product, stacking height, and delivery route. Edge Crush Test values help estimate stacking performance. Burst strength offers another view of puncture and rough handling resistance.
Request samples and test them with the real product inside. A box that survives a warehouse stack may still fail after vibration in a delivery vehicle. Test it honestly.
Flute profiles also change protection and appearance. C flute offers useful cushioning for many shipping cartons. B flute is thinner and can improve printing and storage efficiency. E flute creates a flatter surface for smaller retail packages. Double-wall BC flute adds strength for heavier products, though it uses more material.
Moisture, box dimensions, and internal voids can alter these results. I once approved a strong board for a tall carton, then noticed the wide panels buckled during stacking. The board was not the only problem; the box design needed better geometry.
A dependable packaging partner should explain test methods, provide board data, and accept questions about weak points. Suppliers can be wrong. Good evaluation leaves room to revise the specification.
10 Tips for Choosing Custom Corrugated Packaging
Select Accurate Dimensions and Protective Structural Features
Tip 1: Measure the packed product, not the product alone. Record its length, width, height, and fragile points. Allow only enough clearance for cushioning. Excess space lets items shift during handling. Tight dimensions reduce movement, material use, and unnecessary shipping volume.
Tip 2: Test the box with real products. Corrugated board strength depends on weight, stacking pressure, humidity, and transport conditions. Choose the flute profile and board grade for the actual load. A small trial can reveal crushed corners, weak seams, or difficult packing steps. Computer drawings help, but they cannot show every failure.
Tip 3: Add structural protection where damage is likely. Folded inserts can separate glass, metal parts, or sharp edges. Corner blocks support heavy products. Locking tabs may reduce tape dependence and improve packing consistency. Keep inserts simple enough for workers to install correctly.
Tip 4: Use practical testing before approving production. Perform drop checks from common handling heights and inspect compression after stacking. Look for punctures, panel buckling, and product movement. Moisture exposure may also weaken corrugated board. I have seen a well-designed carton fail because the internal clearance was slightly too generous. That mistake was avoidable. Recheck the prototype after every dimension change.
| No. | Selection Dimension | Recommended Data or Starting Point | Protective Structural Feature | Practical Validation |
|---|---|---|---|---|
| 1 | Measure the product envelope | Record the maximum product length, width, height, weight, and any projecting parts. Use millimetres for consistent calculations. | Design the internal box dimensions around the measured product rather than relying on nominal product dimensions. | Measure at least three samples, including the largest expected unit, and use the maximum verified dimensions. |
| 2 | Allow functional clearance | Begin with approximately 3–6 mm of clearance around rigid, well-protected products; fragile products may require more space for cushioning. | Use a fitted insert, paper cushioning, molded-pulp supports, or foam so the product cannot move freely inside the carton. | Perform a shake test and confirm that the product does not contact the carton walls, corners, or closure area. |
| 3 | Match flute profile to the risk | Typical corrugated flute heights are about 1.5 mm for E-flute, 3 mm for B-flute, 4 mm for C-flute, and 6–7 mm for BC double-wall board. | Choose finer flutes for print quality and small products; choose larger or double-wall flutes for cushioning, stacking, and heavier loads. | Review the carton after compression, vibration, and drop testing to confirm that the board does not buckle or crush. |
| 4 | Specify board strength | Common edge-crush-test selections include approximately 32 ECT for general shipping and 44 ECT or higher for heavier or more demanding applications. | Use stronger liners, higher-strength medium, or double-wall construction when stacking loads, humidity, or long transport routes are expected. | Request the board specification and compare its ECT or equivalent compression rating with the calculated shipping load. |
| 5 | Check stacking compression | Allow for the total weight of cartons stacked above the lowest carton and apply a design safety factor commonly ranging from 3:1 to 5:1. | Use vertical flute orientation, reinforced corners, and a full-overlap or double-bottom construction where stacking is significant. | Conduct a compression test using the expected pallet pattern, load height, storage duration, and environmental conditions. |
| 6 | Protect corners and edges | Keep vulnerable product edges separated from the carton wall by a cushioning zone that is generally at least 10–25 mm for fragile items, subject to testing. | Add corner posts, edge guards, folded end caps, or perimeter pads to absorb concentrated impact forces. | Inspect corners after repeated handling and confirm that product damage does not occur at the first contact points. |
| 7 | Control internal movement | For multi-unit packs, maintain consistent spacing and prevent product-to-product contact; a 6–12 mm separator gap is a useful initial design range. | Use partitions, die-cut dividers, sleeves, or cells sized to the product geometry. | Invert and gently rotate the packed carton to check for shifting, rubbing, noise, or contact between units. |
| 8 | Select an appropriate closure | Use carton-sealing tape commonly supplied in widths of 48–72 mm; heavier cartons may need reinforced tape, stitching, or an adhesive closure. | Use a full-length center seam, reinforced bottom seam, and adequate flap overlap to reduce opening and tear risks. | Apply the closure to clean, dry board and test adhesion after vibration, compression, temperature, and humidity exposure. |
| 9 | Account for moisture and environment | Corrugated board loses strength in high humidity; evaluate performance at the expected storage and transport humidity instead of relying only on dry-room results. | Consider moisture-resistant treatments, liners, pallet covers, or an inner barrier when exposure to condensation or wet handling is possible. | Condition samples before testing and compare compression results in both normal and worst-case environmental conditions. |
| 10 | Validate the complete package | Test the final carton with the actual product, inserts, closure method, weight, pallet pattern, and shipping orientation. | Combine cushioning, structural inserts, reinforced seams, and clear orientation or handling marks where appropriate. | Use a documented sequence of drop, vibration, compression, and climatic tests based on the intended distribution environment, then inspect both package and product. |
Note: The dimensional ranges are practical starting points. Final specifications should be confirmed through package testing because product fragility, distribution hazards, board grade, humidity, and stacking conditions can significantly change the required design.
10 Tips for Choosing Custom Corrugated Packaging
Start with the product’s weight, dimensions, and shipping route. These details guide the right board strength and flute profile. I have seen attractive boxes fail because stacking pressure was ignored. Measure twice. Leave enough room for protective inserts without wasting material.
Treat printing as part of the package structure. Use a clear logo, readable text, and strong contrast on kraft surfaces. Limit colors when possible; excessive ink can weaken visual clarity and increase production complexity. Always request a physical proof before approval. Digital previews can hide color shifts, rough edges, or small text problems. Keep it readable. Choose finishes carefully. A matte coating can create a soft, natural feel, while spot gloss can highlight a logo or product image. However, too many finishes may make recycling more difficult and raise costs.
Ask suppliers about recycled content, responsible fiber sourcing, and water-based or low-impact inks. Request documentation rather than relying on broad environmental claims. Avoid unnecessary plastic laminates when the box does not need extra moisture protection. Design for reuse, but be realistic about how customers will handle the package. Test the finished box in actual conditions, including vibration, humidity, and repeated stacking. I once focused too heavily on sustainability and overlooked warehouse handling; the result needed stronger edges. Good packaging balances brand character, protection, production limits, and measurable environmental choices.
Choose the board structure first, then match printing, branding, finishes, and sustainability options to the product, shipping environment, and budget.
Flute thickness affects cushioning, stacking strength, print surface, and package size. These are typical nominal values; actual specifications vary by board construction and manufacturer.
For custom packaging, confirm the required board grade, edge-crush performance, moisture resistance, ink system, coating or varnish, recycled-fiber content, and recyclability before approving the final design.
When choosing custom corrugated packaging, compare suppliers through measurable evidence, not attractive samples. Request board grade, flute profile, recycled content, manufacturing capacity, and quality records. FEFCO’s 2023 statistics reported more than 51 billion square metres of corrugated board production in Europe, showing the scale of this supply chain. Large capacity does not always mean better service. Ask for pre-production samples and verify dimensions with calipers. Test the sample.
Testing standards should match the shipping environment. Edge Crush Test helps estimate stacking strength, while burst strength evaluates resistance to puncture and tearing. ASTM D4169 or ISTA 3E can simulate vibration, compression, and repeated handling. ISO 12048 is also useful for compression testing. A professional supplier should provide test conditions, conditioning time, and laboratory results. Numbers can mislead. A high ECT rating may still fail when moisture softens the board.
Compare total cost, not only the unit quotation. Include dies, printing plates, setup charges, minimum order quantities, storage, and rejected units. The U.S. Census Bureau reported e-commerce sales of over 1.1 trillion dollars in 2024, increasing pressure on packaging availability and delivery speed. Request a written schedule covering artwork approval, sampling, production, inspection, and shipment. Build a safety buffer of several days. I have seen projects delayed because artwork approval was treated as administrative work. That gap matters. Suppliers should explain material substitutions before production, not after a truck is booked. Review delivery performance quarterly, because the cheapest quote can become expensive after delays, damage, and emergency freight.